Based on the RockPlus MOM Manufacturing Operations Management Platform, Hegong Software built, for the leading domestic CMP manufacturer, an integrated digital system spanning "production execution" to "laboratory quality management", with RockPlus MES + RockPlus LIMS at its core.
The project was organized around four directions:
Equipment interconnection, production processes, SPC quality control, and MES-LIMS data collaboration.
1. RockPlus MES + LIMS: an integrated manufacturing and quality platform
RockPlus MES runs shop-floor production execution; RockPlus LIMS runs laboratory quality management.
RockPlus MES covers:
- Production orders and work order management
- Process routing and operation management
- Raw material and finished goods logistics
- PDA scanning and in-line pass-through
- Automatic equipment data collection
- Cutting tool, fixture, and equipment management
- Production quality management
- Full product traceability
- ERP system integration
RockPlus LIMS covers:
- Inspection task management
- Laboratory equipment management
- Test report management
- SPC / CPK statistical analysis
- WECO Rule automatic out-of-control detection
- OCAP non-conformance handling
- DCC controlled document management
- Inspection data and quality report management
MES and LIMS are not two isolated systems; they are linked around the same product and the same batch.
Key production parameters generated during casting and curing can flow into LIMS quality reports; laboratory results such as density, hardness, thickness, and compressibility can in turn participate in MES production release, label printing, and product shipment.
The result is a single data chain:
Product → Manufacturing process → Equipment parameters → Raw materials → Laboratory testing → Quality results
2. Equipment interconnection: 12 production steps and diverse equipment types brought online
Equipment interconnection is a core workstream of the project.
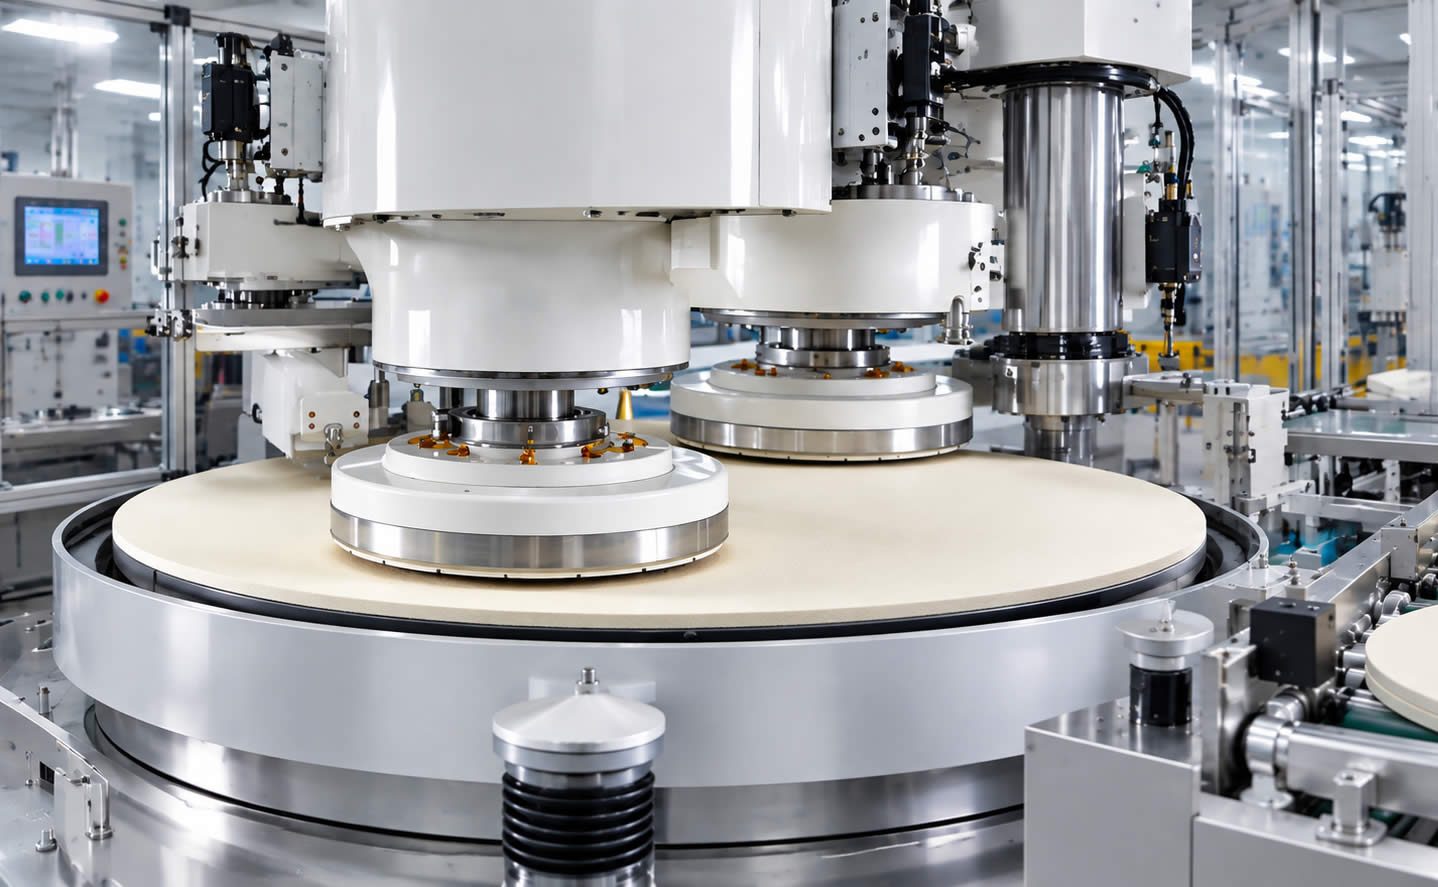
Centered on the CMP polishing pad process flow, RockPlus MES uniformly connects and collects data from equipment across preheating, casting, curing, slicing, laser marking, sanding, engraving, cleaning, 3D inspection, lamination, labeling, and in-line inspection.
To handle the inconsistent device interfaces on site, the system supports multiple industrial communication and data-acquisition methods:
- PLC communication
- Modbus TCP
- OPC
- FANUC FOCAS
- In-line inspection equipment interfaces
- PDF test-report parsing
- Access database parsing
- Serial-port and instrument data collection
- MES pushing barcodes and production instructions to equipment
For example, at the casting step, MES collects agitation temperature, speed, pressure, degassing time, melt temperature, and raw material flow rates; at the curing step it records curing temperature, time, mold and layer-position information; at engraving it obtains machining parameters, tool information, and vacuum pressure through device communication; and at lamination it binds liner and adhesive batches, roller temperature, air pressure, and tension into the production record.
Through unified interconnection, data previously scattered across PLCs, CNCs, inspection devices, and manual logs is automatically accumulated into MES and associated with the corresponding product and production batch. Equipment collection spans multiple core steps and diverse production-equipment types.
3. Production processes: "one item, one code" through the entire CMP pad manufacturing flow
RockPlus MES uses production work orders and product barcodes as the backbone to connect the whole manufacturing process.
The overall flow:
ERP sales order / production order → MES work order management → material preparation and raw material registration → PDA scan verification → preheating → window fabrication → pre-mixing → casting → curing → slicing → laser marking → sanding → inspection → engraving / cleaning → lamination → labeling → final inspection → packaging → finished-goods receiving → shipment → ERP data write-back
At every key step, the system automatically builds the relationship between product and manufacturing resources through barcodes, PDAs, and equipment data collection.
For example:
- Raw materials are scan-verified before entering production;
- Casting automatically associates equipment process parameters;
- Curing binds molds and production layer positions;
- Slicing creates the semi-finished product barcode;
- The laser marker automatically receives marking instructions pushed by MES;
- Engraving, slicing, and sanding enforce tool life and on-machine verification;
- Lamination binds auxiliary material models and batches;
- Finished labels and case codes complete warehousing and shipment.
This forms a genuine "one item, one code, code through the whole line". The full process and its forward/reverse traceability design are consistent with the actual implementation.
4. LIMS: bringing laboratory test data into the manufacturing quality system
For the many test items and complex instruments of CMP pads, the project manages all laboratory testing through RockPlus LIMS.
The system covers multiple test report types, including:
- MOCA purity
- Incoming material inspection
- Full density
- Density
- Hardness
- Thickness
- Compressibility
- Peel force
- SEM imaging
- Air permeability
- Light transmittance
- Groove
- Product slice data
- Casting batch production parameters
- Curing batch production parameters
For different instruments, RockPlus LIMS uses different data-access methods according to each device's characteristics.
For example, hardness testers and thickness gauges have their output reports parsed; the universal testing machine's test data is read from the device's database file; SEM, optical profilometers, density meters, and other inspection instruments are integrated automatically or semi-automatically according to their interface capability.
The system turns laboratory instruments from "standalone test devices" into key data sources of the manufacturing data framework, so test results are archived and traced uniformly by product, batch, and work order. LIMS covers density, hardness, thickness, compressibility, SEM, groove, purity and more physical and material tests.
5. SPC + WECO Rule: from outcome inspection to statistical process control
Given the high demands on batch stability and product consistency for semiconductor advanced materials, the project made SPC a core part of quality management.
RockPlus LIMS establishes a three-layer SPC system.
Product SPC
Continuous statistical analysis of key product quality indicators:
density, hardness, thickness, compressibility, SEM imaging
Equipment SPC
Process capability analysis of production and equipment-related indicators:
casting, curing, slicing, groove, air permeability, light transmittance
Raw Material SPC
Trend monitoring of critical raw material indicators:
MOCA purity
On top of conventional SPC control limits, the system further introduces the WECO Rule out-of-control detection mechanism.
The system identifies potential anomalies automatically from the position, trend, and distribution of successive data points.
This means that even if a test result is still within specification, the system produces out-of-control records as soon as the data exhibits sustained drift, consecutive one-sided distribution, or other abnormal trends.
Once an SPC out-of-control signal appears, it can enter the OCAP handling workflow, forming a complete record of cause, action, and result.
The resulting quality loop:
Test data → Real-time SPC analysis → WECO Rule automatic detection → Anomaly trigger → OCAP handling → Action records → Continuous SPC/CPK analysis
The project thereby shifts quality management from "deciding pass/fail after production" to continuous monitoring and early warning of manufacturing process stability. WECO Rules, SPC/CPK, and the OCAP loop are integral parts of the project's quality system.
6. First-article gating and poka-yoke: pulling quality control onto the shop floor
In key machining steps, RockPlus MES further establishes on-site error-proofing and first-article gating.
For example, when a product enters 3D inspection, the system automatically obtains groove depth, width, and pitch results.
If the first article fails inspection, the system can lock subsequent production, preventing batch machining while the process is in an abnormal state.
Meanwhile, engraving, slicing, sanding, and trimming enforce tool model, usage-count, and life management, with verification at tool loading.
Quality control thus extends from the laboratory and final inspection to equipment and the production process itself:
errors prevented in advance, anomalies intercepted in time, and complete process data trail.
7. MES-LIMS collaboration: full forward and reverse traceability
Through the collaboration of RockPlus MES and RockPlus LIMS, the project established a complete traceability chain spanning raw materials, manufacturing, laboratory testing, and finished-goods shipment.
Forward traceability
From a finished product barcode, one can query:
Production order → All process steps → Processing equipment → Process parameters → Raw material batches → Auxiliary materials → Tools/fixtures → Inspection data → Packaging and shipping records
Reverse traceability
When a quality anomaly or customer complaint occurs, one can trace backward from the product to:
Production batch → Casting batch → Curing batch → Equipment parameters → Raw material batches → Inspection data
helping quality and process engineers quickly narrow the scope and providing data for root-cause analysis and continuous process improvement.
8. Bi-directional ERP integration: linking planning, production, inventory, and shipment
RockPlus MES is also integrated bi-directionally with the customer's ERP system.
ERP synchronizes to MES:
- Item master data
- Sales orders
- Production work orders
- Finished goods shipping plans
MES reports back to ERP:
- Raw material registration and consumption
- Inventory data
- Finished goods receiving
- Finished goods issue and latest inventory
forming the closed loop:
Sales order → Production plan → Manufacturing execution → Material consumption → Finished goods receiving → Product shipment
eliminating double entry and information gaps between ERP and the shop floor.








 Back to List